One shop, from flat sheet to finished part
PS Laser makes precision sheet metal components for industrial and OEM customers. Parts are cut on our fiber lasers or Amada turret punches, formed on a CNC press brake, welded and assembled, then powder coated on our own line. One team plans and checks the job from your drawing to dispatch.
CNC Fiber Laser Cutting
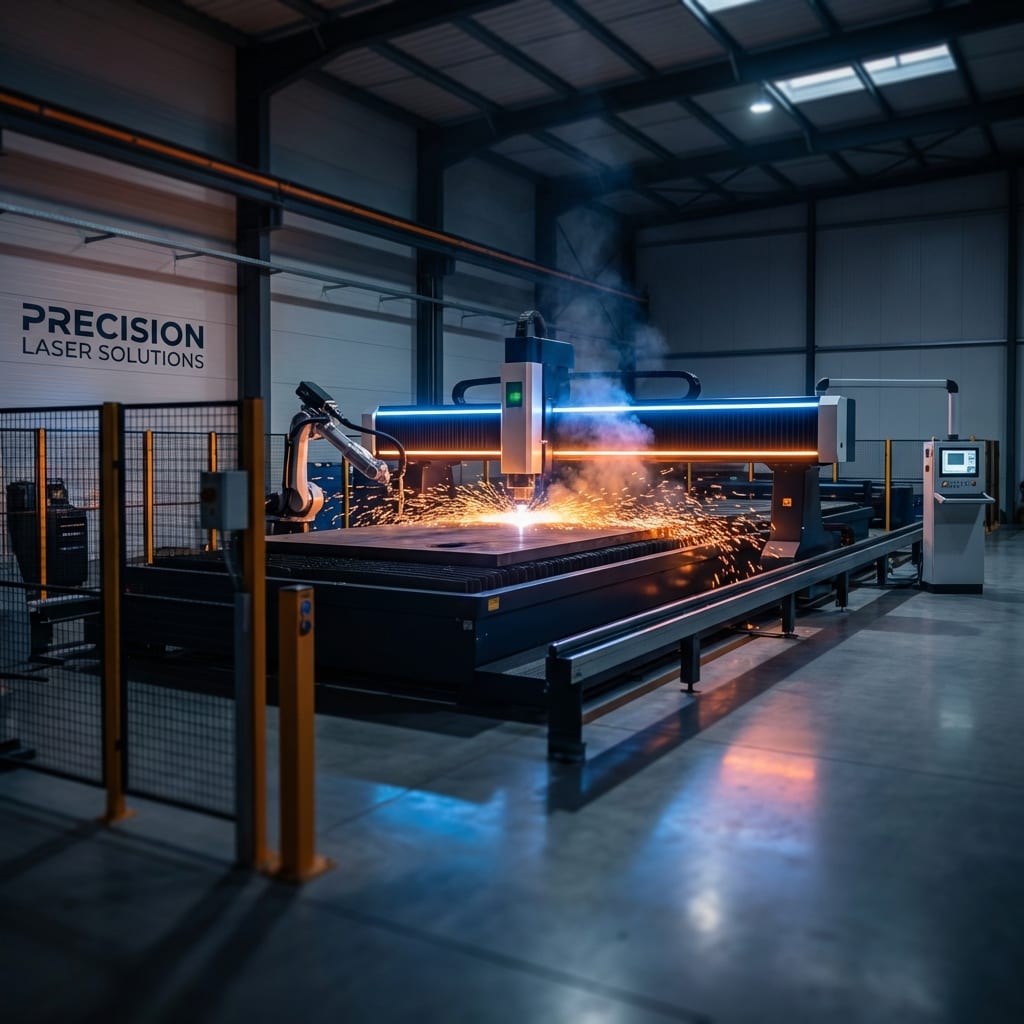
Our cutting cell runs two fiber lasers, each with a 3 m x 1.5 m bed. The 3 kW HSG machine takes the thicker plate and production batches; the 1.5 kW Genesis handles thin sheet and fine, detailed profiles.
Send us a DXF and we nest it, program it and cut it. The result is a clean edge and accurate holes and slots, ready for bending, welding or coating in the same shop.
Machines
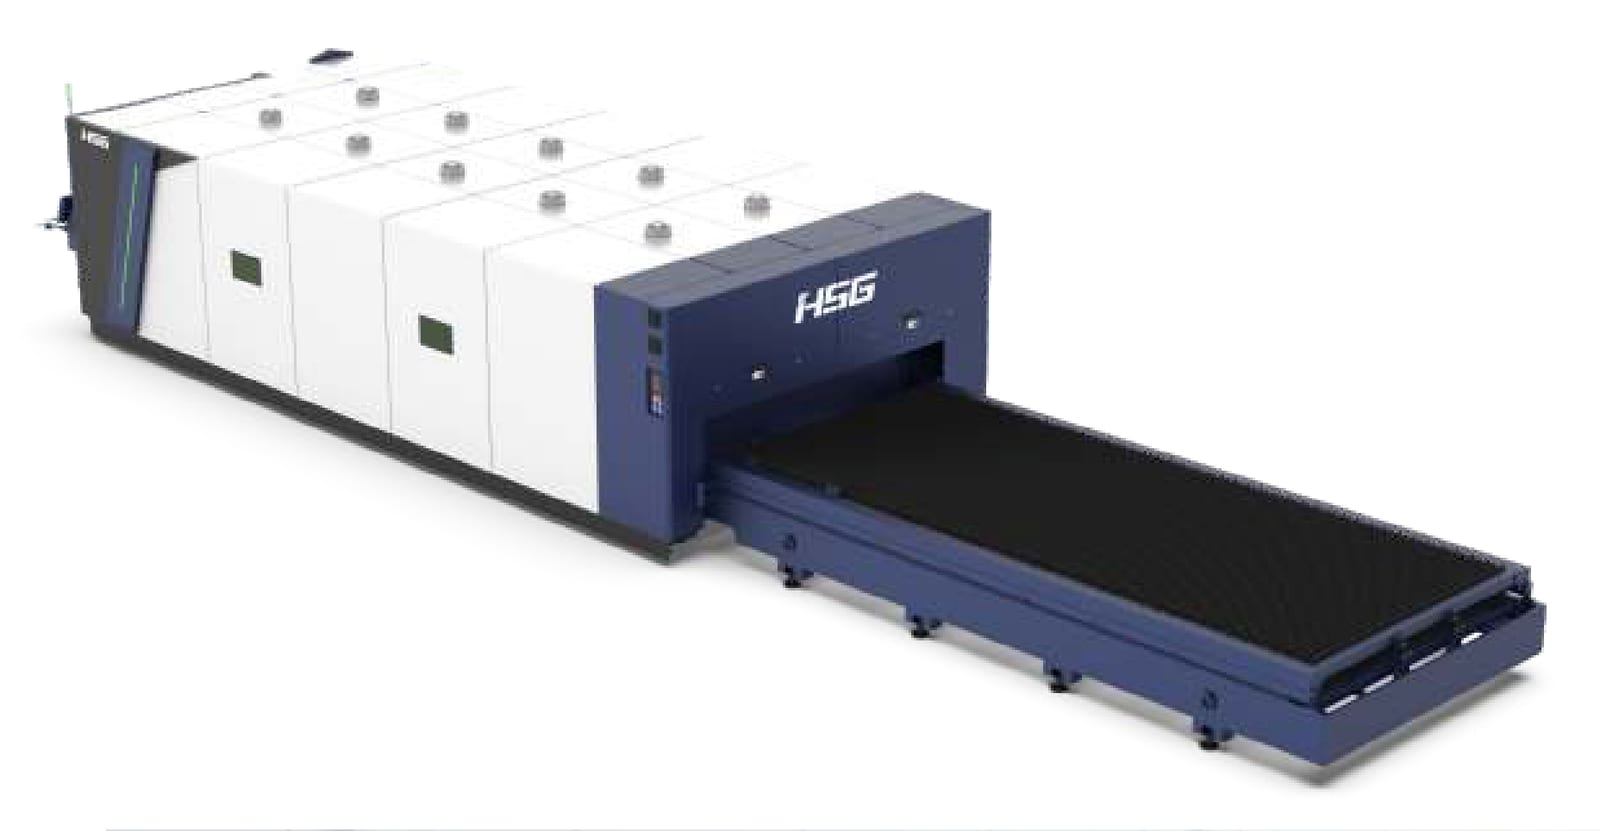
HSG 3 kW Fiber Laser Cutting Machine
Manufacturer image of the model we run- 3 kW fiber laser
- Bed 3 m x 1.5 m
- Enclosed cabinet with exchange table
- MS 16 mm · SS 12 mm · Al 8 mm · Brass/Cu 4 mm
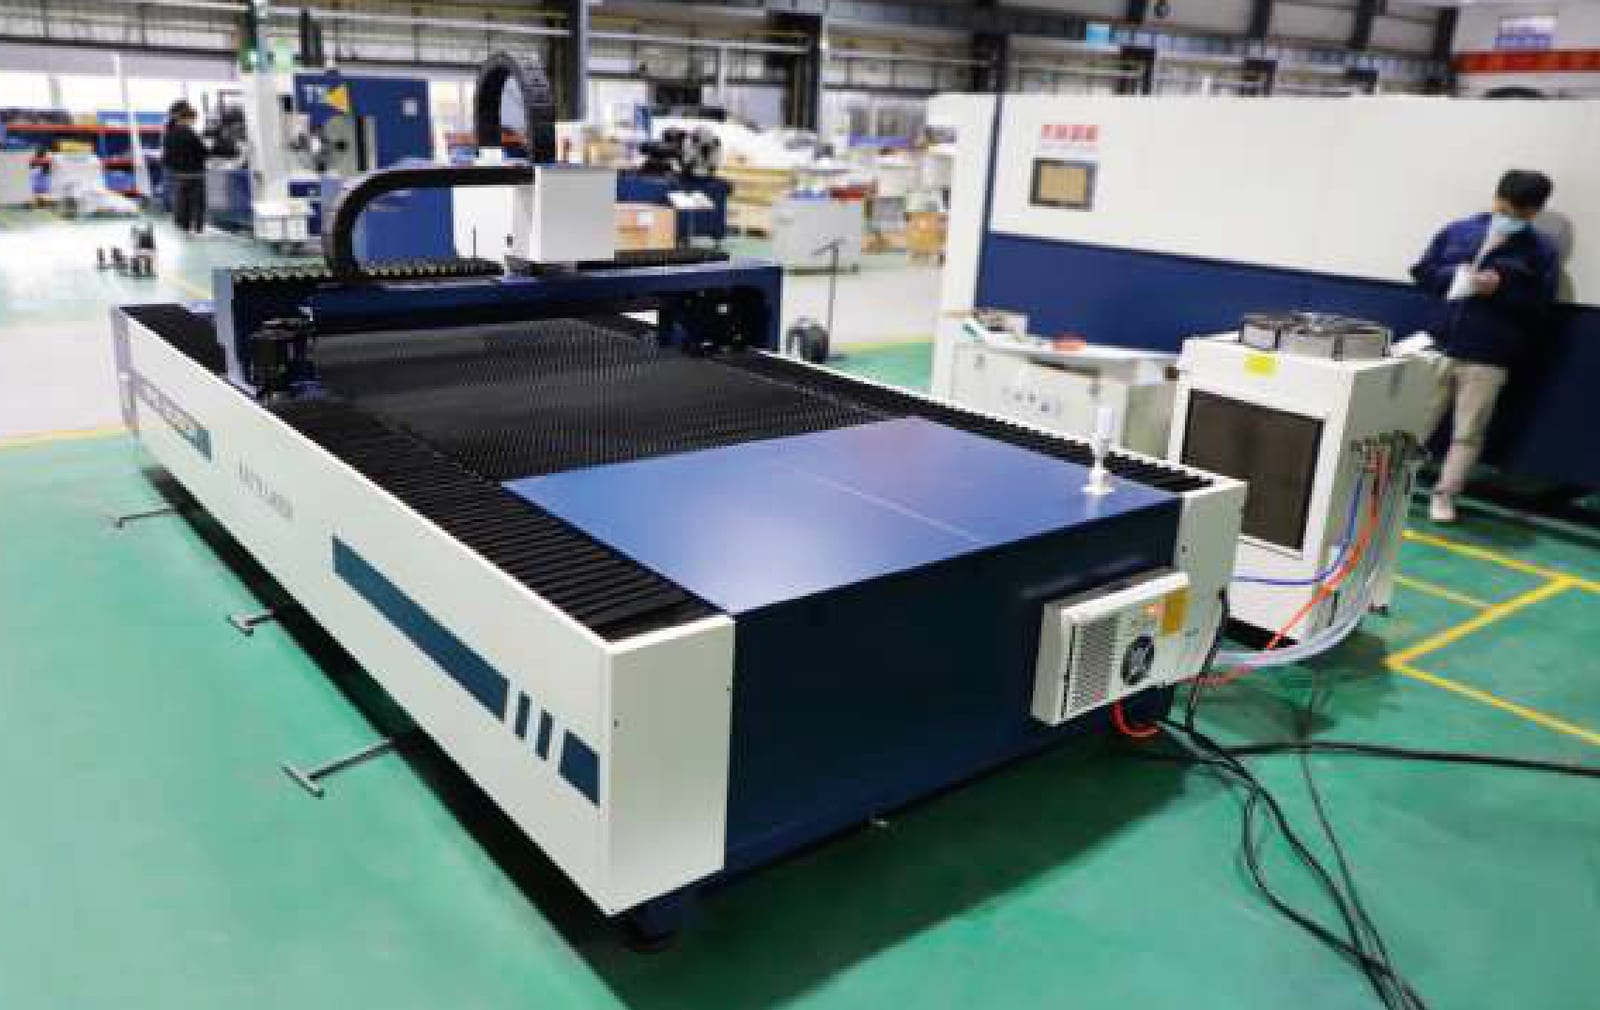
Genesis 1.5 kW Fiber Laser Cutting Machine
Manufacturer image of the model we run- 1.5 kW fiber laser
- Bed 3 m x 1.5 m
- Open-bed gantry
- Ideal for thin sheet & fine profiles
Capacity
- Mild Steel
- up to 16 mm
- Stainless Steel
- up to 12 mm
- Aluminium
- up to 8 mm
- Brass
- up to 4 mm
- Copper
- up to 4 mm
- Sheet size
- 3 m x 1.5 m bed
Typical applications
- Enclosure and panel blanks
- Brackets, gussets and base plates
- Machine guards and covers
- Laser-cut jaali and decorative panels
- Flat parts for fabrication and assembly
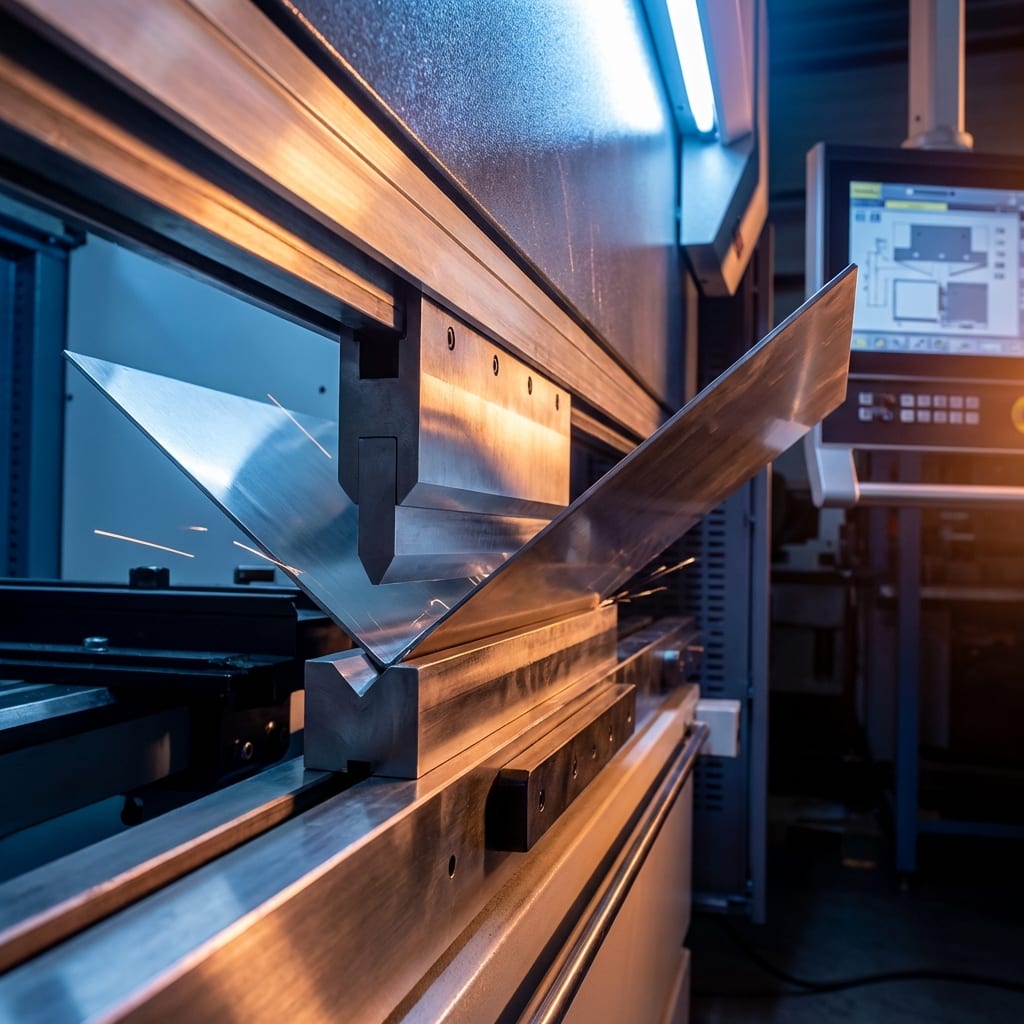
CNC Bending
A 175 Ton CNC press brake with a 3 m working length forms the parts cut on our lasers. It handles sheet from 1 mm up to 12 mm.
Bend sequences are programmed and checked before the first part. Because blank development happens in-house, the flat pattern and the finished bend are designed together, so parts come out at the right size.
Machine
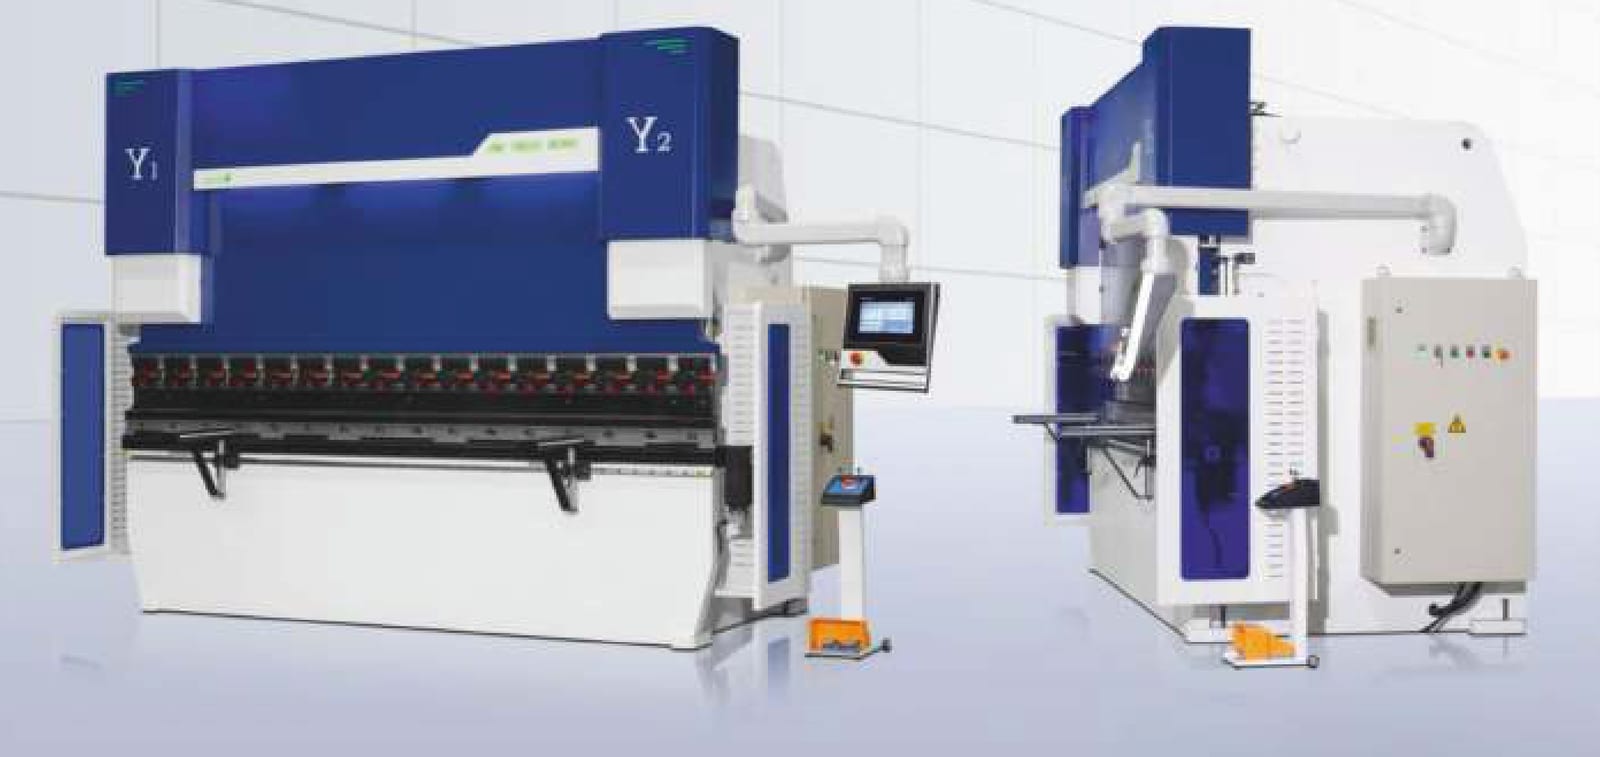
CNC Press Brake 175 Ton x 3 m
Manufacturer image of the model we run- 175 Ton capacity
- 3 m bending length
- Sheet thickness 1–12 mm
- CNC Y1/Y2 synchro axes
Capacity
- Press force
- 175 Ton
- Bending length
- up to 3 m
- Sheet thickness
- 1 – 12 mm
Typical applications
- Enclosures, boxes and control panel bodies
- Channels, angles and U-sections
- Brackets and mounting plates
- Covers, trays and doors
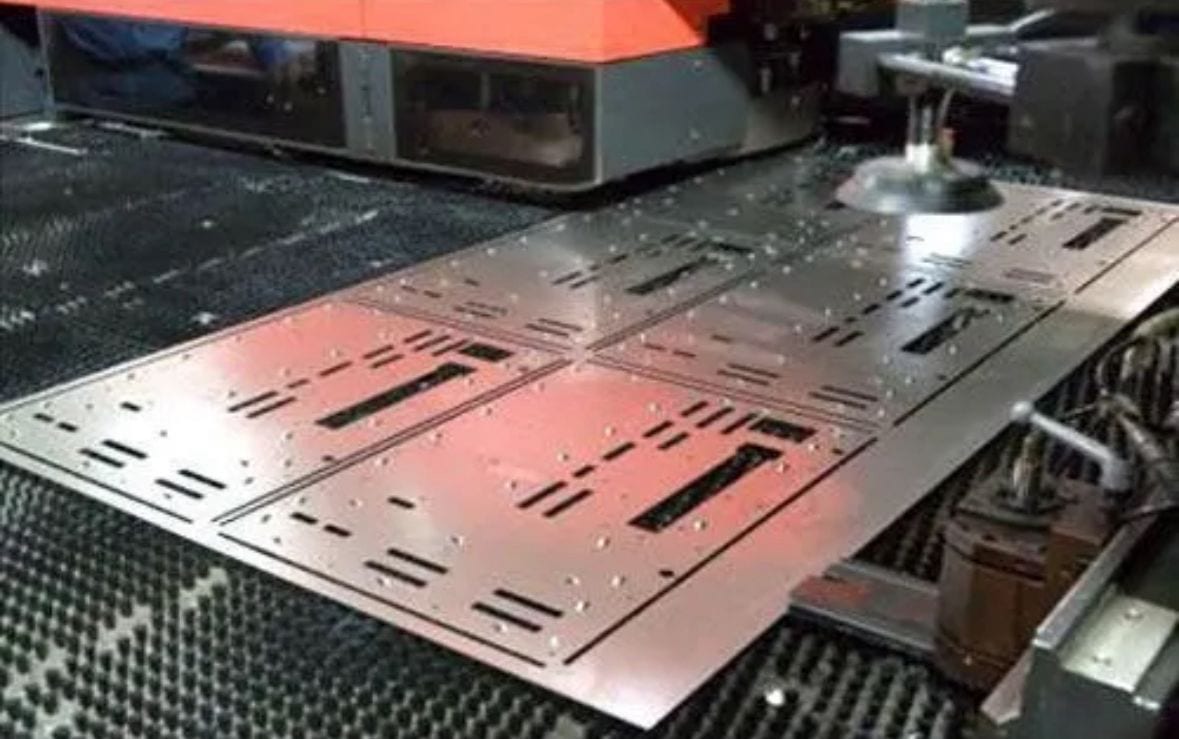
CNC Turret Punching
Two Amada CNC turret punches cover repetitive holes, slots, knock-outs and perforations. On parts with many identical features, punching is often faster and cheaper than laser cutting.
The 32 Ton VELA II runs 40 tool stations on an 8 x 4 ft table. The 16 Ton PEGA covers lighter sheet on a 4 x 4 ft table.
Machines
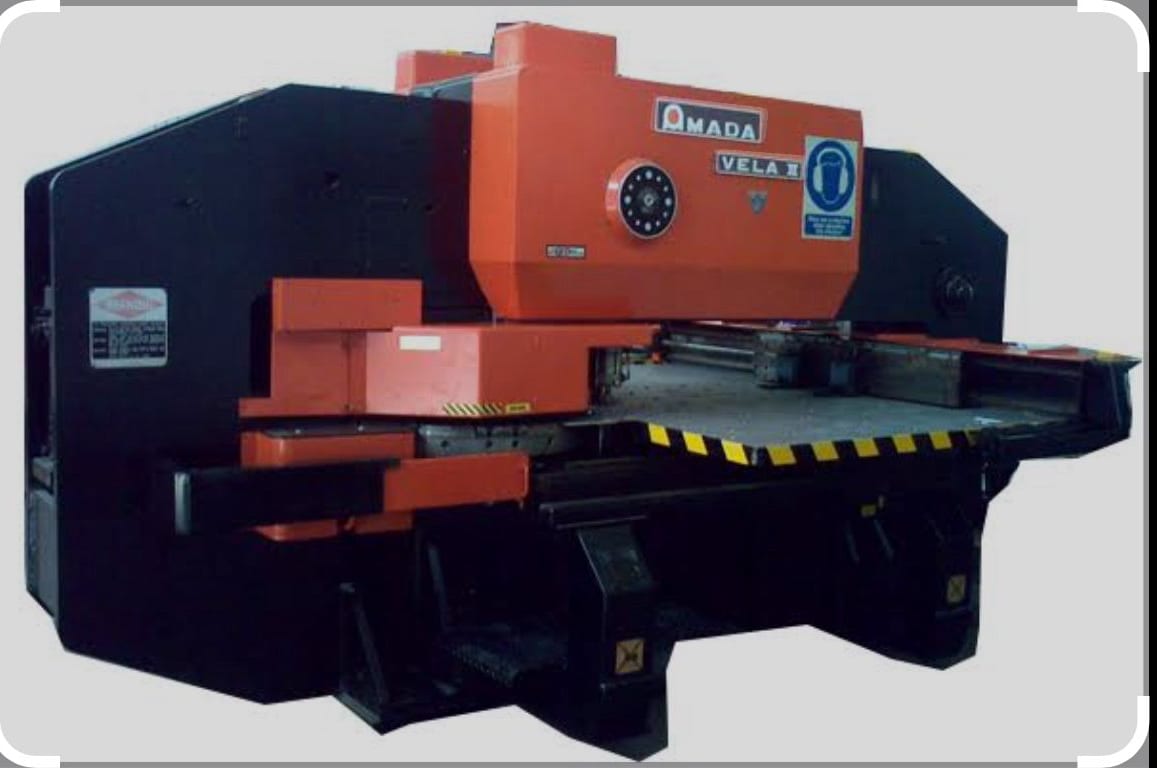
Amada VELA II CNC Turret Punch – 32 Ton
Manufacturer image of the model we run- 32 Ton
- Punching up to 5 mm
- 40 stations
- Table 8 ft x 4 ft
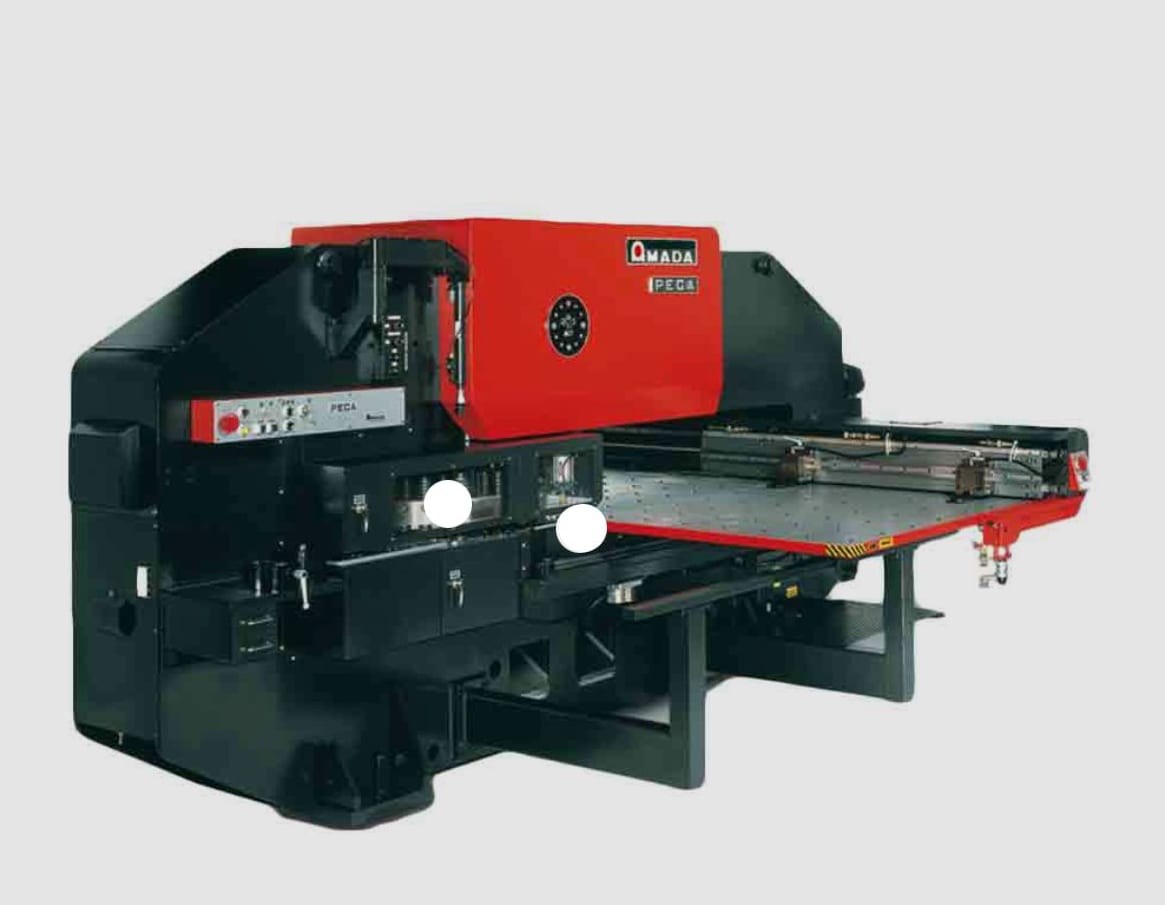
Amada PEGA CNC Turret Punch – 16 Ton
Manufacturer image of the model we run- 16 Ton
- Punching up to 3 mm
- 26 stations
- Table 4 ft x 4 ft
Capacity
- Amada 32 T
- up to 5 mm · 40 stations · 8 x 4 ft
- Amada 16 T
- up to 3 mm · 26 stations · 4 x 4 ft
Typical applications
- Perforated sheets and ventilation patterns
- Electrical panel and enclosure cut-outs
- Cabinet grills
- High-volume flat parts with repeated holes
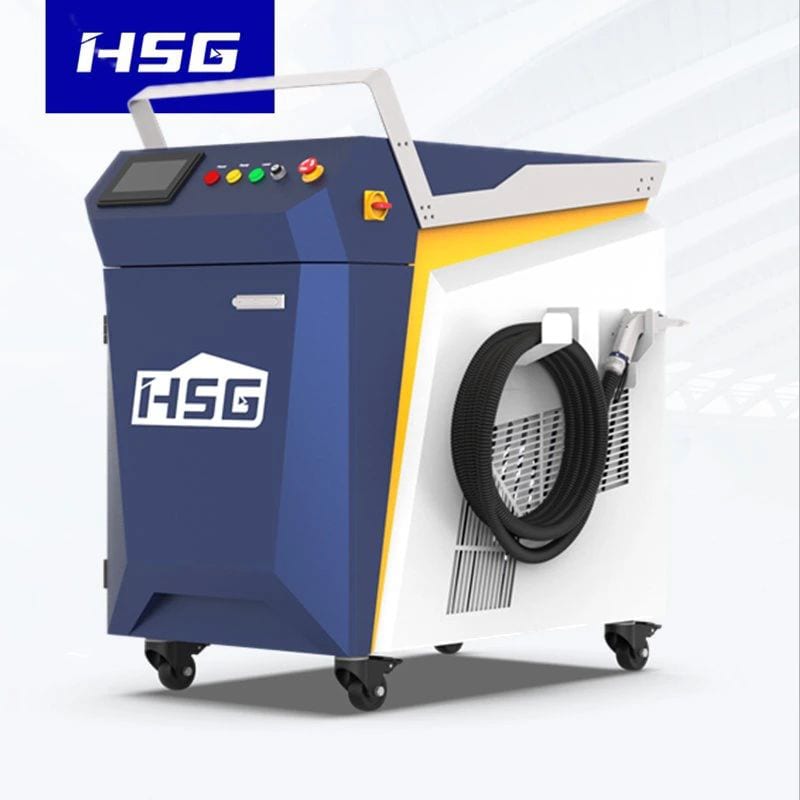
Laser Welding
Our HSG 1.5 kW handheld laser welder puts in a narrow, concentrated heat zone. You get neat seams with less distortion and less grinding afterwards than conventional welding usually leaves.
We weld mild steel, stainless steel and aluminium, including fillet, vertical, tailor and flat joints. It suits visible joints on enclosures and on stainless steel work.
Machine
HSG 1.5 kW Handheld Laser Welding Machine
Manufacturer image of the model we run- 1.5 kW handheld laser
- MS, SS & Aluminium
- Fillet, vertical, tailor & flat welds
- Clean, low-distortion seams
Capacity
- Materials
- MS, SS & Aluminium
- Weld types
- Fillet, vertical, tailor, flat
Typical applications
- Enclosure corners and seams
- Stainless steel cabinets and trays
- Thin-sheet assemblies where distortion matters
- Visible joints that need a clean finish
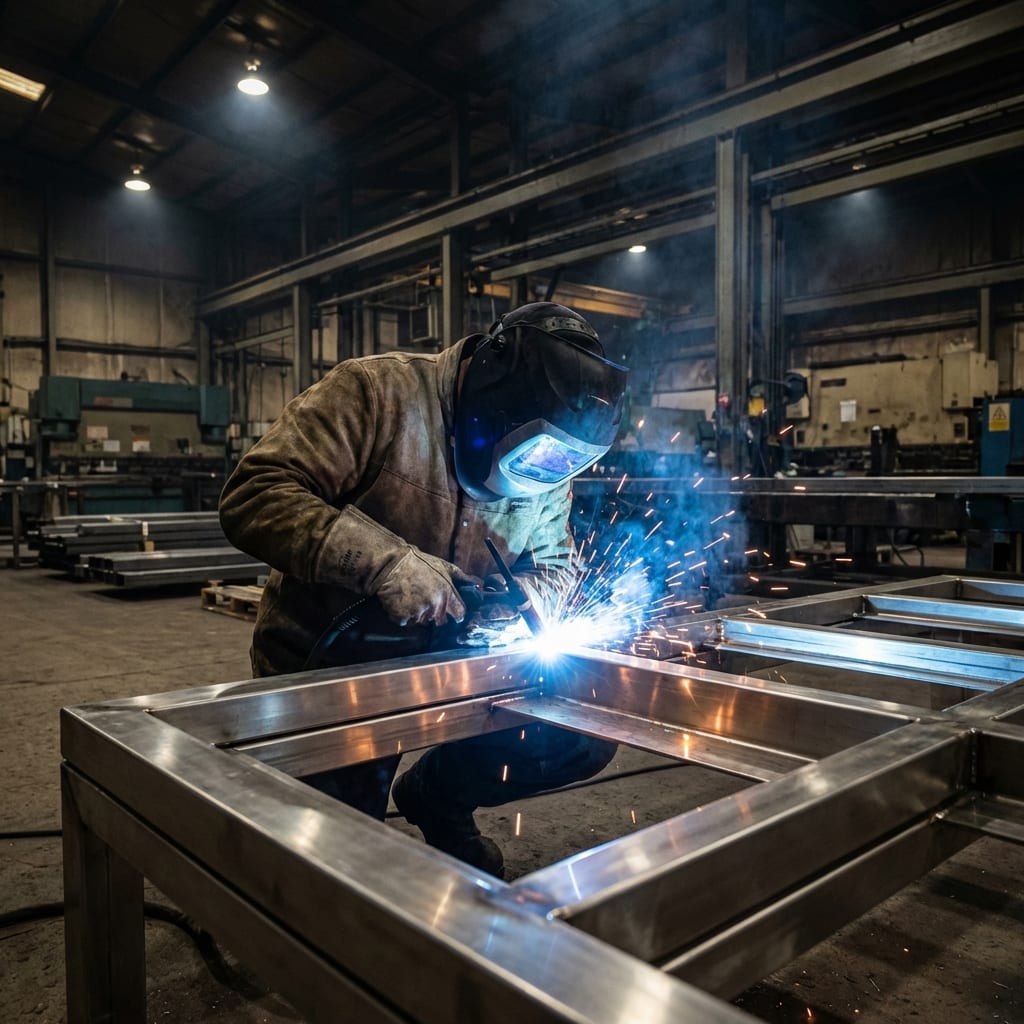
Sheet Metal Fabrication & Welding
Cut and bent parts are joined into finished assemblies at dedicated welding stations for mild steel, stainless steel and aluminium. Welding clamps and fixtures keep repeat parts consistent.
Soft welding, grinding, buffing and cleaning are done in-house, so assemblies arrive ready for powder coating or ready to install.
Fabrication facilities
- Dedicated welding stations for MS, SS & Aluminium
- Welding clamps and fixtures for repeat jobs
- Soft welding
- Grinding, buffing and cleaning
- In-house tool designing & manufacturing
Typical applications
- Frames, stands and structures
- Control panel and enclosure assemblies
- Welded fixtures and jigs
- Machine guards and covers
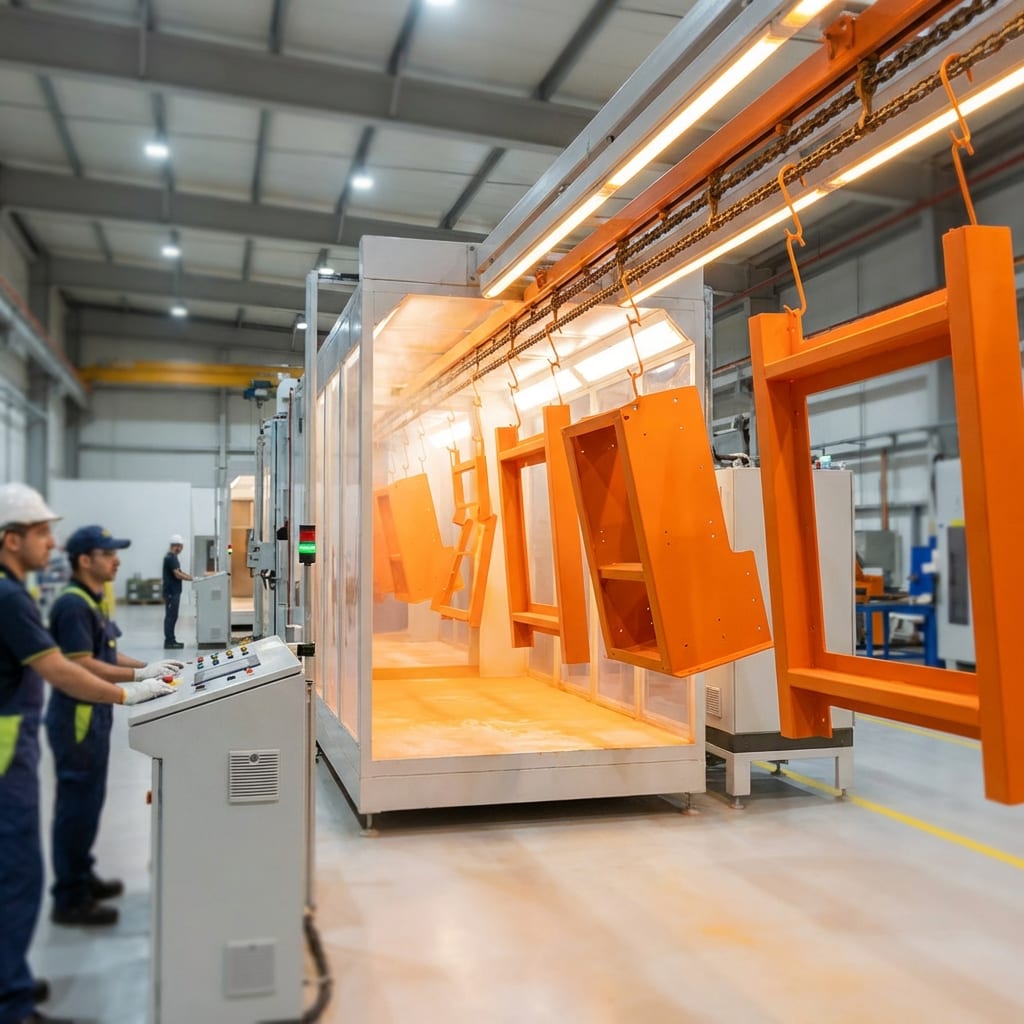
Powder Coating
Our PLC-based powder coating plant puts parts through a 9-tank pre-treatment process and an oven dry at 120 °C. They are then sprayed with a Wagner gun in a stainless steel booth and cured in an oven.
The SS booth lets us change colour quickly, which keeps small batches practical. Parts finished on this line sustain 900–1000 hours in salt spray testing.
Machine
PLC-Based Powder Coating Plant
Representative image- 9-tank pre-treatment
- Oven drying 120 °C & oven curing
- SS booth with Wagner gun
- 900–1000 hrs salt spray
Capacity
- Pre-treatment
- 9-tank process
- Drying
- Oven drying at 120 °C
- Booth
- SS booth, Wagner gun
- Salt spray
- 900–1000 hours
Typical applications
- Enclosures and control panels
- Architectural and decorative panels
- Brackets, frames and fabricated parts
- Cabinet grills and accessories
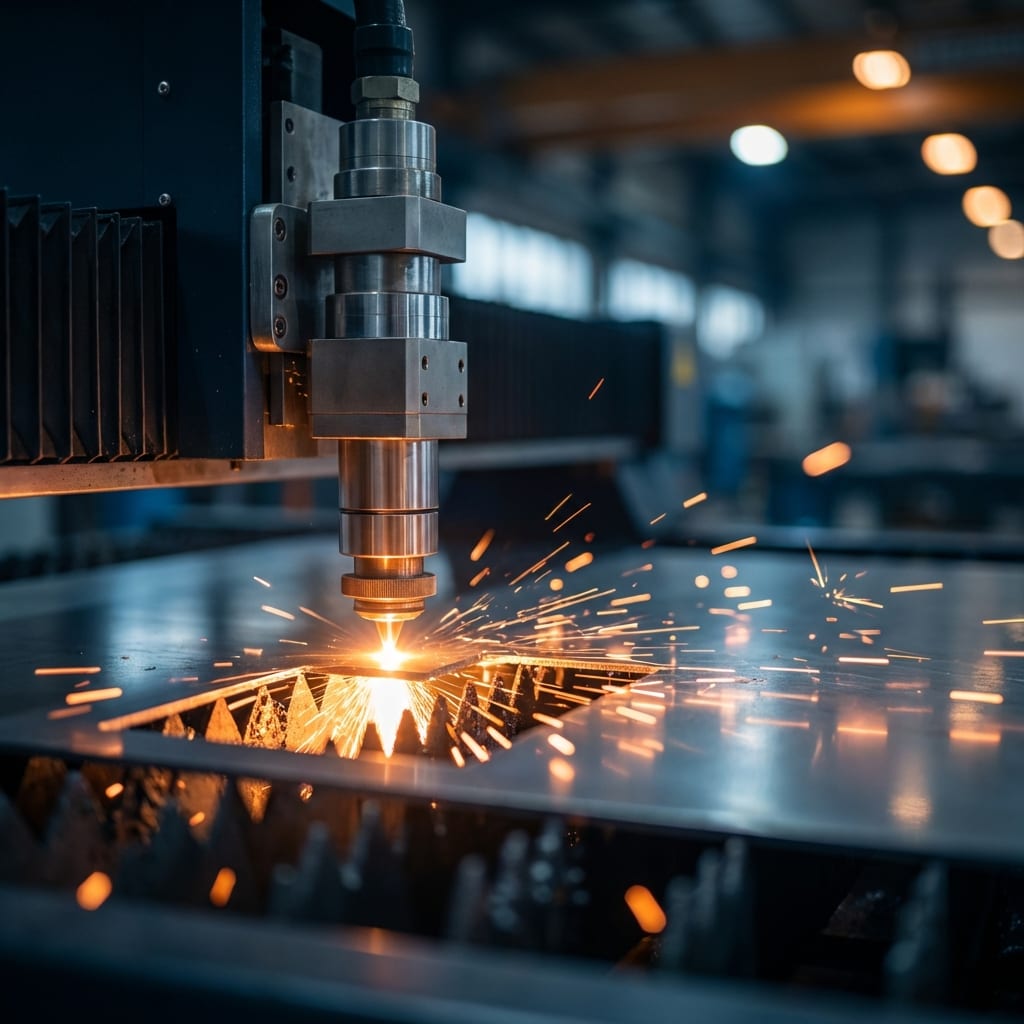
Design & CAM Support
We follow a system approach: 3D modelling, drafting, CAM modelling, rendering, nesting and laser programming all happen in-house before a sheet goes on the machine.
If you only have a sketch, a sample or a 3D model, we can work out the flat pattern, check the bends and program it for production.
Software we use
- Production Designer: sheet metal part development, bending simulation, blank development
- Sheet Works: sheet metal parts and 3D modelling
- Blank CAM: nesting and laser cutting programming
Typical applications
- Converting drawings and samples to DXF
- Flat-pattern (blank) development for bent parts
- Nesting to reduce material waste
- Design help from concept to installation
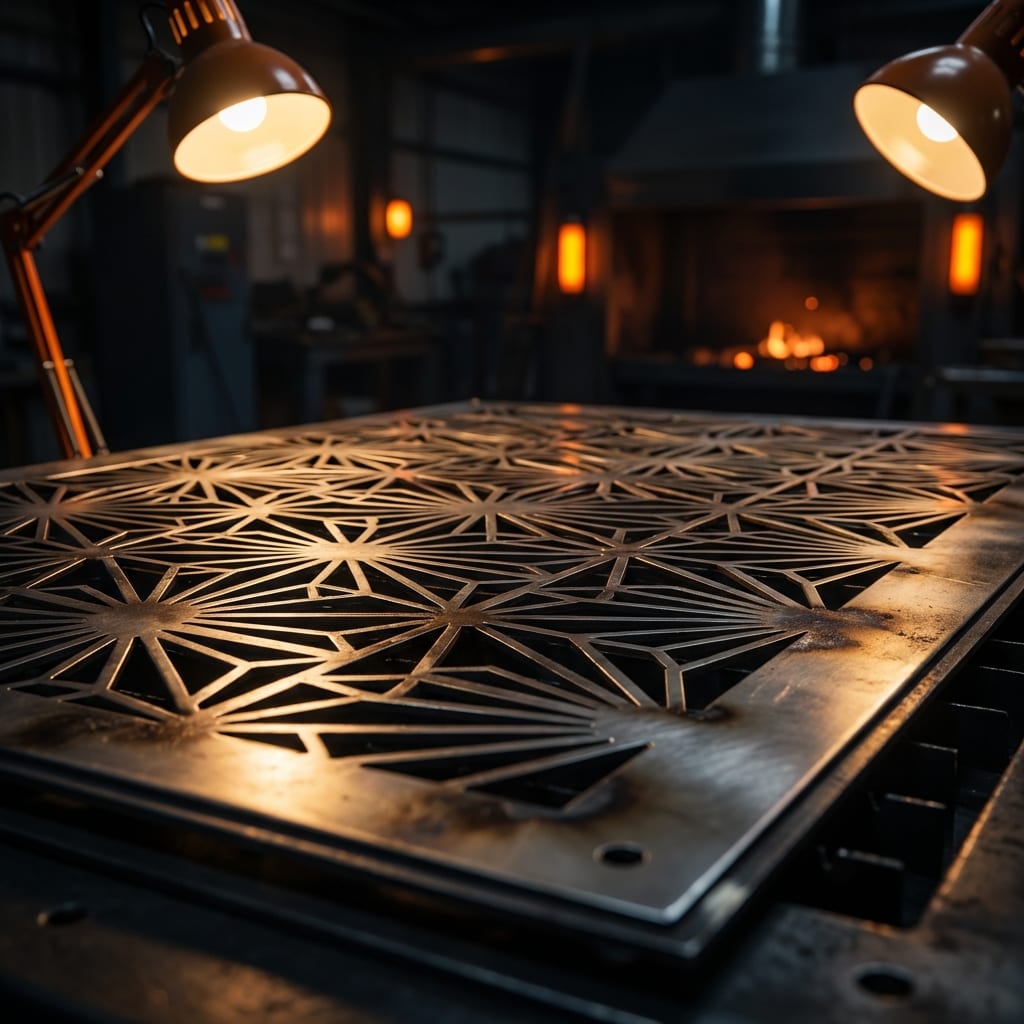
Architectural, Grills & Job Work
The same lasers, press brake and powder coating line also make jaali screens, decorative panels, cabinet grills and accessories, and architectural job work.
Image: representative work
Materials We Cut
Maximum laser cutting thickness for each material on our fiber lasers (3 m x 1.5 m bed).
Mild Steel up to 16 mm
Structural parts, brackets, enclosures. Usually powder coated.
Stainless Steel up to 12 mm
Corrosion-resistant parts, food and outdoor use, visible finishes.
Aluminium up to 8 mm
Lightweight covers, panels and housings.
Brass up to 4 mm
Decorative inlays, nameplates and fittings.
Copper up to 4 mm
Electrical parts and decorative accents.
Bending: 1–12 mm on the 175 T x 3 m press brake. Turret punching: up to 5 mm (32 T) and 3 mm (16 T). Not sure what to specify? Read our guide to choosing material and thickness.
From Drawing to Dispatch
Every job moves through one shop, so nothing waits on an outside supplier.
- 01
Design & Planning
CAD/CAM programming and material planning.
- 02
Laser Cutting
Precision CNC laser cutting with fiber technology.
- 03
Punching & Bending
Amada turret punching and CNC press brake forming.
- 04
Welding & Assembly
Laser welding and fabrication on dedicated stations.
- 05
Powder Coating
9-tank pre-treatment, coating and oven curing.
- 06
Quality & Dispatch
Inspection, packaging and delivery.
Have a drawing ready?
Send your DXF or drawing on WhatsApp with the material, thickness and quantity, and we will come back with a quote.